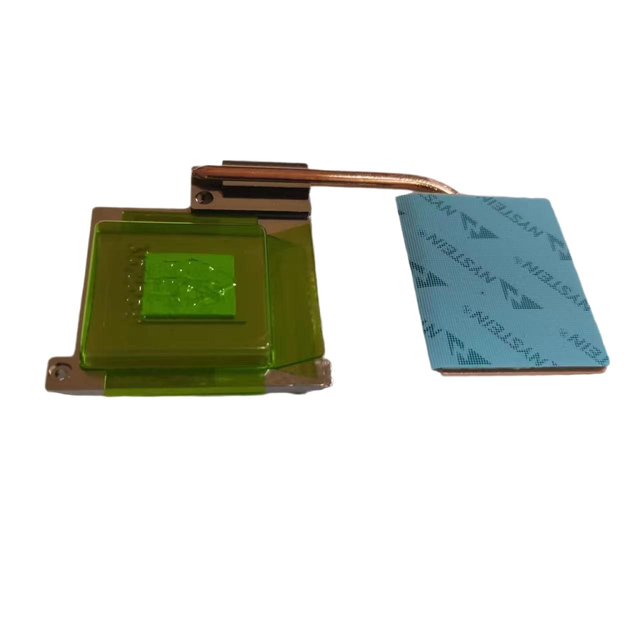
A seamless copper tube is formed and fitted into a machined aluminum base (AL6061/6063), carrying coolant beneath the heat sources while the base provides mounting and heat spreading. The tube is mechanically retained and thermally bonded to minimize interface resistance, then the assembly is leak and flow validated. Tube routing, bend geometry and diameter are set against your cooling coverage and hydraulic resistance.
Assembled vs. monolithic vs. embedded-tube. An assembled cold plate is built by joining separate parts — a machined base, a cover, and integrated copper tubes, heat pipes or fin packs — sealed with mechanical fasteners, epoxy, or O-ring seals. This modular route keeps initial cost and tooling low and lets the layout change quickly between prototype iterations, at a low-to-moderate heat-load rating. A monolithic cold plate (FSW, vacuum-brazed, or deep-drilled) is machined from a single sealed body for higher heat flux; an embedded-tube plate presses or solders a tube into a base groove. If your goal is design flexibility, quick re-spins and a cost-effective solution for moderate heat, an assembled cold plate is the right fit.
High-conductivity copper carries coolant directly.
Lightweight base for mounting and heat spreading.
Mechanically retained, thermally bonded.
Bend geometry matched to component layout.
Airtightness and flow validation per plate.
| Base Material | Aluminum base + copper tube (embedded tube) |
|---|---|
| Cooling Circuit | Machined channels / integrated copper tube, heat-pipe or fin-pack routing |
| Assembly Method | Separate parts joined by mechanical fasteners, epoxy bonding, or O-ring / elastomer seals |
| Internal Architecture | Machined base + cover with integrated copper tube / heat-pipe / fin-pack routing |
| CNC Machining Tolerance | As tight as +/-0.005 mm on milling / drilling |
| Dimensional Inspection | Hexagon CMM +/-0.001 mm; 2.5D optical projector |
| Leak Testing | 100% in-house airtightness leak detection (LCP testers) |
| Flow Validation | Two-stage flow-resistance measurement; in-house thermal test lab |
| Surface Treatments | Anodizing, passivation, precision sandblasting |
| Quality System | ISO 9001:2015; IATF 16949:2016 |
| Capacity | 60,000+ thermal parts per year |
| Lead Time | Typical samples 7-15 days; production scheduled to volume |
Note: the table lists KingKa's verified assembled cold plate build options and capabilities. Final geometry, channels, ports and finish are confirmed against your drawing.
KingKa controls every step of the assembled cold plate build in-house, from incoming-material inspection to final CMM sign-off. The workflow below reflects the modular split-part assembly used for this cold plate.
Design & CFD. 3D Pro/E layout with CFD thermal review sizes the cooling circuit and balances flow for the target heat load.
CNC machining. The base and cover are machined to +/-0.005 mm, with channels, mounting holes and ports matched to your drawing.
Part preparation. Copper tubes, heat pipes or fin packs are formed and fitted to the base routing for the selected cooling path.
Assembly & sealing. The separate parts are joined and sealed - mechanical fasteners, epoxy bonding, or O-ring / elastomer seals - into the final module.
Leak & flow validation. Every assembly passes 100% airtightness leak detection and two-stage flow-resistance testing.
Dimensional CMM inspection. Hexagon CMMs (to +/-0.001 mm) verify dimensions, mounting holes and ports against your CAD.
100% airtightness leak detection - dedicated LCP leakage testers confirm every assembly.
Two-stage flow-resistance testing - channels clear and pressure-stable.
Hexagon CMM & 2.5D projector - dimensional verification to +/-0.001 mm against your drawing.
Seal & joint inspection - fastener torque, bond coverage and O-ring seating verified per plate.
Surface-finish control - anodize / passivation / sandblasting verified for corrosion and contact.
Embedded copper tube cold plates suit low-to-medium power-density applications needing high-conductivity coolant routing:
Power electronics
Motor controllers
Inverters
Industrial equipment
Battery and EV modules
Provide your heat-source layout, coolant and flow budget. KingKa routes the copper tube, embeds it in the base and validates to your drawing and acceptance criteria.
For buyers, KingKa is a direct manufacturer with 16+ years of thermal-production experience, 50+ CNC centers (3-/4-/5-axis) and a stated 60,000+ parts per year, certified to ISO 9001:2015 and IATF 16949:2016. Engineering support includes in-house CFD thermal simulation, FEA and 3D Pro/E design before tooling.
From drawing to volume. Send your STEP/CAD file and thermal budget for an assembly design proposal matched to your heat load and cost target.
Flexible supply. Prototypes typically 7-15 days; production scheduled to your forecast.
One quality system. Prototype, pilot and production all carry 100% leak and CMM inspection.
R&D backing. Dongguan Nancheng R&D center supports channel/fin/tube design, validation and scale-up.