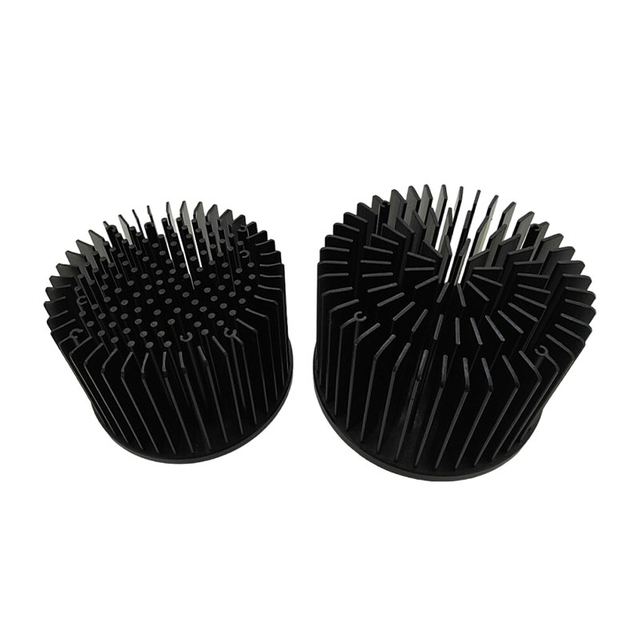
The body is cold forged from AL1070 with the pin field and the flange in one piece, then the flange is turned to diameter, the bayonet notches are milled, and the base face is faced flat. The part is black anodized and sealed. Notch position and depth are held to the mating seat, since a bayonet that binds is worse than a screw. What a pin field does to airflow is covered in what is a pin heat sink.
Twists into the seat, no screws in the fins.
Surface without a bond line.
Tip gap differs from root gap.
Isolation and emissivity in one finish.
Seats flat in the holder.
| Base Material | Aluminum 1070, cold forged, black anodized |
|---|---|
| Base | Round flange with bayonet notches |
| Pin Field | Forged, slight radial lean |
| Finish | Black anodized, sealed |
| Material | Aluminum 1070 |
| Base CNC Tolerance | Milling / drilling / tapping down to +/-0.005 mm |
| Dimensional Inspection | Hexagon CMM +/-0.001 mm; 2.5D optical projector |
| Quality System | ISO 9001:2015; IATF 16949:2016 |
| Capacity | 60,000+ thermal parts per year |
| Lead Time | Samples typically 7-15 days; production scheduled to volume |
Note: values above are KingKa build options and verified capability; final geometry, holes and finish are confirmed against your drawing.
A bayonet notch is a fit, not a feature: the angular position and the ramp angle decide whether the part locks or rattles. Both are cut after forging, from the seat drawing rather than from the sink outline.
Design & CFD. 3D layout with CFD review sizes the fin field, pipe route and base thickness to the load and airflow.
Base machining. Plate, pockets and pipe channels are milled on 50+ CNC centers to +/-0.005 mm.
Fin and pipe joining. Fins skived, stacked or extruded; pipes pressed and soldered; the stack joined to the base by the process the design calls for.
Face fly-cutting. Contact face machined flat after joining so the part sits true on the device.
Final inspection. Hexagon CMM (+/-0.001 mm) and 2.5D projector check critical features; 4-stage IQC / IPQC / FQC.
Fin pitch and height - measured against the drawing before packing.
Base flatness - fly-cut face checked on the contact side.
CMM report - critical dimensions to +/-0.001 mm.
Joint inspection - solder or weld fillet checked along the stack feet.
Visual and batch audit - IQC / IPQC / FQC on every run.
Notched-base sinks suit fixtures with a bayonet seat:
Lamp and luminaire assemblies
Downlight and track heads
Camera housings
Industrial light engines
Retrofit LED modules
Send the seat drawing - diameter, notch width, notch angle and insertion depth. KingKa forges the body and cuts the notches to that seat, then anodizes to the colour you need. Where the flange is square and no bayonet is needed, the square pin grid heat sink is the match.
KingKa is a direct manufacturer with 16+ years in thermal production, 50+ CNC centers, in-house skiving, FSW and vacuum brazing, certified to ISO 9001:2015 and IATF 16949:2016.
Send the mating seat drawing, not only the sink drawing - the notches are dimensioned from the seat, and a sink drawing without it cannot be checked.
One supplier for the whole assembly. Base, fins, pipes and hardware under one quality system.
CFD before tooling. Design review catches a bad layout before metal is cut.
Prototype to volume. Samples in 7-15 days, production scheduled to forecast.