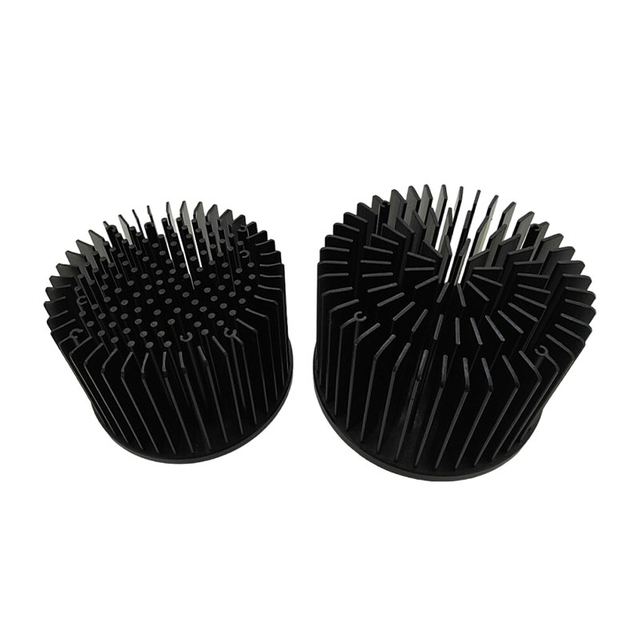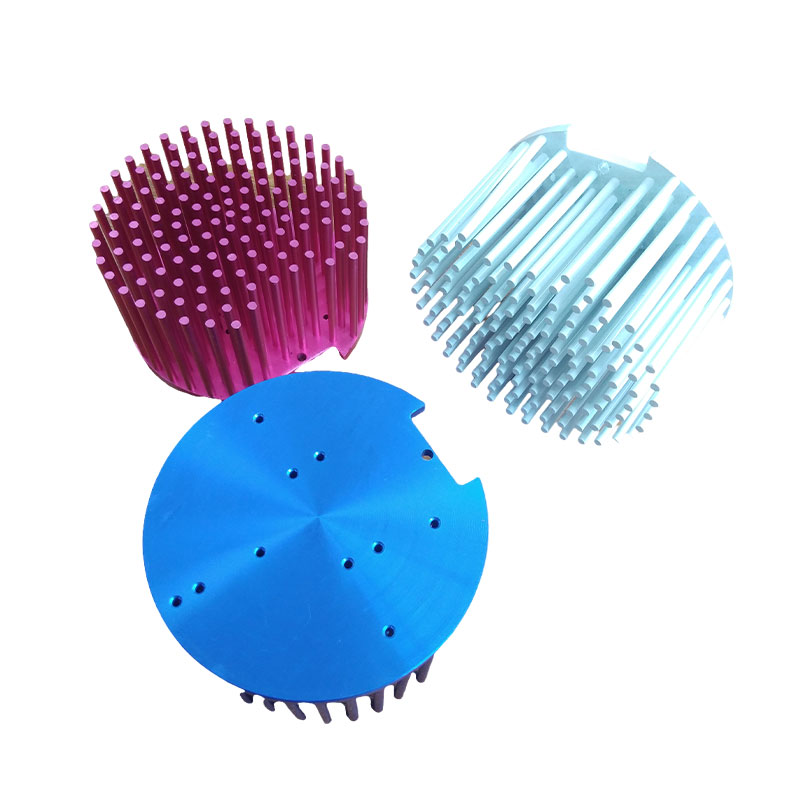


The sink is cold forged from AL1070 at room temperature, work hardened in the die, then machined for the base face, centre features and fixing points. The part is cleaned and phosphated before electrophoretic coating: the whole body is immersed, the coating is deposited electrically including into the fin gaps, and the film is then cured. Colour is set in the bath, so a batch carries one colour. The difference between a coating and an anodic film is compared in the anodized heat sink guide.
Housing match without masking.
Film reaches into the gaps, not just the outside.
Fin gaps stay open.
Darker films help in still air.
Outdoor and industrial fixtures.
| Base Material | Aluminum 1070, cold forged, electrophoretic coated |
|---|---|
| Material | Aluminum 1070 |
| Thermal Conductivity | 226 W/m-K (AL1070) |
| Coating | Electrophoretic (E-coat), colour per batch |
| Coating Coverage | Full part including fin flanks |
| Base CNC Tolerance | Milling / drilling / tapping down to +/-0.005 mm |
| Dimensional Inspection | Hexagon CMM +/-0.001 mm; 2.5D optical projector |
| Quality System | ISO 9001:2015; IATF 16949:2016 |
| Capacity | 60,000+ thermal parts per year |
| Lead Time | Samples typically 7-15 days; production scheduled to volume |
Note: values above are KingKa build options and verified capability; final geometry, holes and finish are confirmed against your drawing.
E-coating is a line process, not a bench process: colour comes from the bath and film thickness from the voltage. That is why colour is quoted per batch, and why a mid-series colour change carries a setup rather than a per-part cost.
Design & CFD. 3D layout with CFD review sizes the fin field, pipe route and base thickness to the load and airflow.
Base machining. Plate, pockets and pipe channels are milled on 50+ CNC centers to +/-0.005 mm.
Fin and pipe joining. Fins skived, stacked or extruded; pipes pressed and soldered; the stack joined to the base by the process the design calls for.
Face fly-cutting. Contact face machined flat after joining so the part sits true on the device.
Final inspection. Hexagon CMM (+/-0.001 mm) and 2.5D projector check critical features; 4-stage IQC / IPQC / FQC.
Fin pitch and height - measured against the drawing before packing.
Base flatness - fly-cut face checked on the contact side.
CMM report - critical dimensions to +/-0.001 mm.
Joint inspection - solder or weld fillet checked along the stack feet.
Visual and batch audit - IQC / IPQC / FQC on every run.
E-coated forged sinks are chosen where the fixture is seen and the environment is hostile:
High-power LED fixtures
Automotive lighting
Industrial and warehouse lighting
Outdoor and street lighting
Consumer electronics
Send the outline, the fin height, the fixing points and the colour target (RAL or a sample). KingKa confirms the coating on a coupon before the batch, then forges and coats to that reference. Where the same body is anodized instead of coated, the part is the round anodized pin fin sink.
KingKa is a direct manufacturer with 16+ years in thermal production, 50+ CNC centers, in-house skiving, FSW and vacuum brazing, certified to ISO 9001:2015 and IATF 16949:2016.
Send the colour reference with the drawing - a RAL number or a physical sample - because the bath is set once per run and a colour matched by eye on a screen will not repeat.
One supplier for the whole assembly. Base, fins, pipes and hardware under one quality system.
CFD before tooling. Design review catches a bad layout before metal is cut.
Prototype to volume. Samples in 7-15 days, production scheduled to forecast.