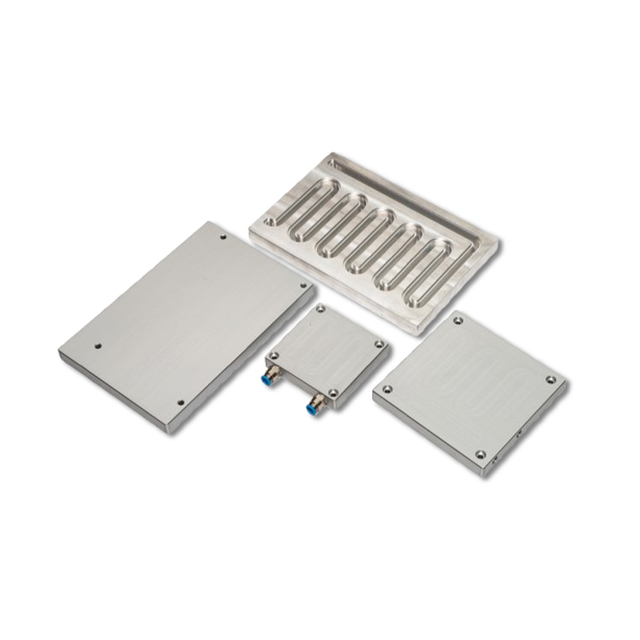
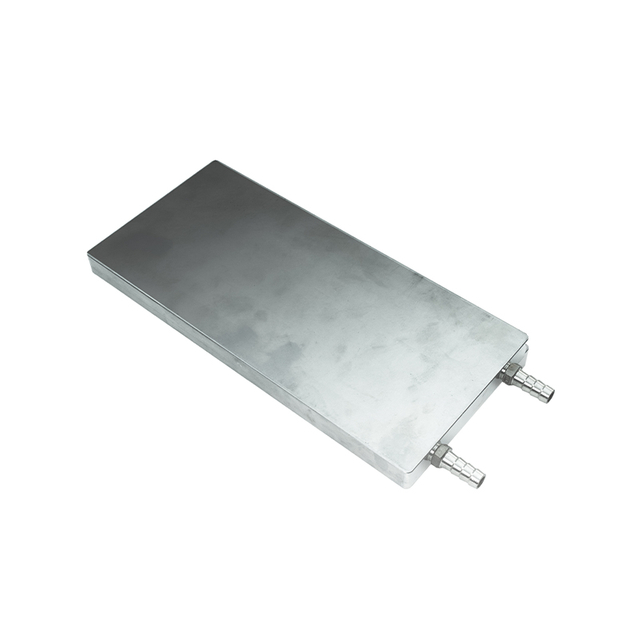
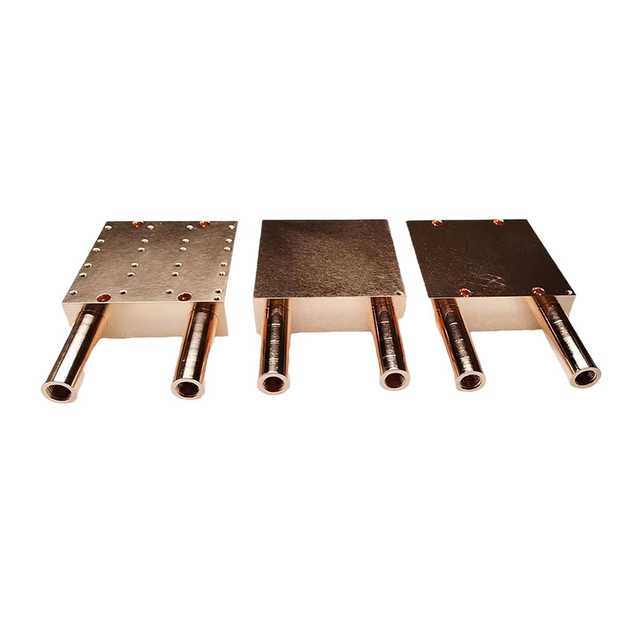
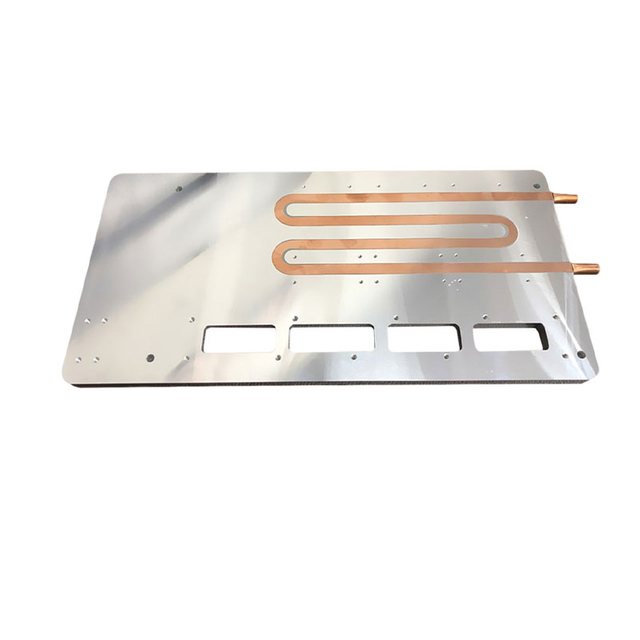
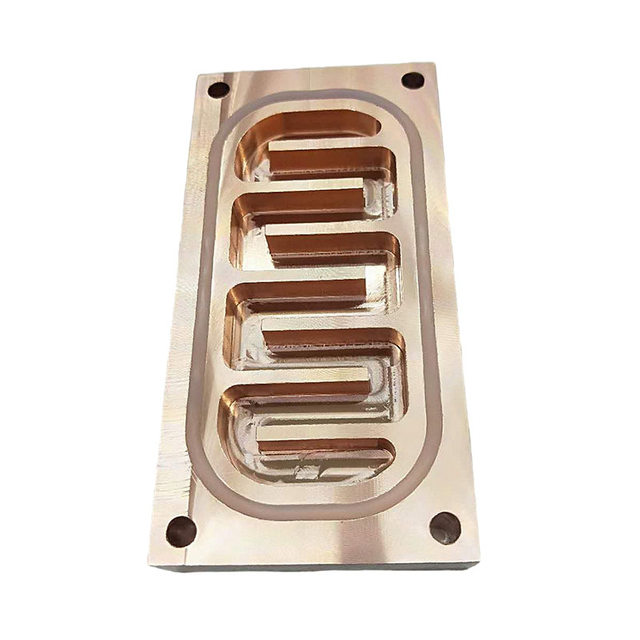
Plates are produced to your specified size in Aluminum 6061/6063 or Copper 1100. Channels and ports are CNC-milled across the full envelope, and the cover is FSW-sealed along the weld path. Size does not compromise the process - the same solid-state seal, machining tolerances and validation apply from small to large plates.
Compact modules through large-format plates.
Leak-free welding across the full size range.
Machined features to your drawing at any scale.
Aluminum or copper for your thermal and weight targets.
Validated regardless of plate size.
| Base Plate Material | Aluminum / Copper (to drawing) |
|---|---|
| Cooling Circuit | CNC-machined channels, solid-state FSW-sealed |
| Joining Technology | Solid-state Friction Stir Welding (FSW) - no flux, no filler metal |
| CNC Machining Tolerance | As tight as +/-0.005 mm (high-speed milling / turning) |
| Dimensional Inspection | Hexagon CMM +/-0.001 mm; 2.5D optical projector |
| Leak Testing | 100% airtightness leak detection (4 x LCP leakage testers) |
| Flow Validation | Two-stage flow-resistance test |
| Surface Control | Fly-cut / ground mounting face; Kett film-thickness & roughness testers |
| Quality System | ISO 9001:2015; IATF 16949:2016 |
| Coolant Handling | Airtight-cleaned, residue-free channels; coolant matched to your system |
| Lead Time | Typical samples 7-15 days; production scheduled to volume |
Note: the table lists KingKa's verified build options and capabilities. Final geometry, passes, ports and finish are confirmed against your drawing.
KingKa controls every step of the build in-house, from incoming-material inspection to final flow testing. The workflow below reflects the FSW construction used for this liquid cold plate.
Thermal design & DFM. 3D Pro/E layout and CFD review of the internal channels before any metal is cut, so the flow path matches your heat map and pressure-drop budget.
CNC channel machining. Channels, fins and port features are milled in the aluminum or copper base on 50+ CNC centers (3-/4-/5-axis), then the cover plate is positioned for welding.
Friction Stir Welding. A rotating tool forges the cover to the base below the melting point on two China-Aerospace FSW machines - a flux-free, solid-state seal with no porosity path.
Finish & validation. The welded plate is fly-cut flat, then every assembly passes 100% airtightness leak detection and a two-stage flow-resistance test before CMM dimensional sign-off.
100% airtightness leak detection - four dedicated LCP leakage testers confirm every assembly.
Two-stage flow-resistance test - channels are clear and pressure-stable.
Hexagon CMM & 2.5D projector - dimensional verification to +/-0.001 mm against your drawing.
Airtight internal cleaning - residue-free channels ready for your coolant.
Salt-spray & Kett film/roughness - corrosion and surface-finish validation per batch.
Custom-size FSW plates cover the envelopes standard products cannot:
Data-center racks and large servers
Battery packs and energy storage
Large power converters
Industrial machinery
Any application needing a non-standard envelope
Send your envelope, heat map and coolant conditions. KingKa confirms manufacturing feasibility for the size, designs the channel network and FSW-seals the plate to your drawing.
For buyers, KingKa is a direct manufacturer with 16+ years of thermal-production experience, 50+ CNC centers (3-/4-/5-axis) and a stated 60,000+ parts per year, certified to ISO 9001:2015 and IATF 16949:2016. Engineering support includes in-house CFD thermal simulation and 3D design before tooling.
From drawing to volume. Send your STEP/CAD file and thermal budget for a CFD-backed proposal.
Flexible supply. Prototypes typically 7-15 days; production scheduled to your forecast.
One quality system. Prototype, pilot and production all carry 100% leak and CMM inspection.
R&D backing. Dongguan Nancheng R&D center supports design, validation and scale-up.