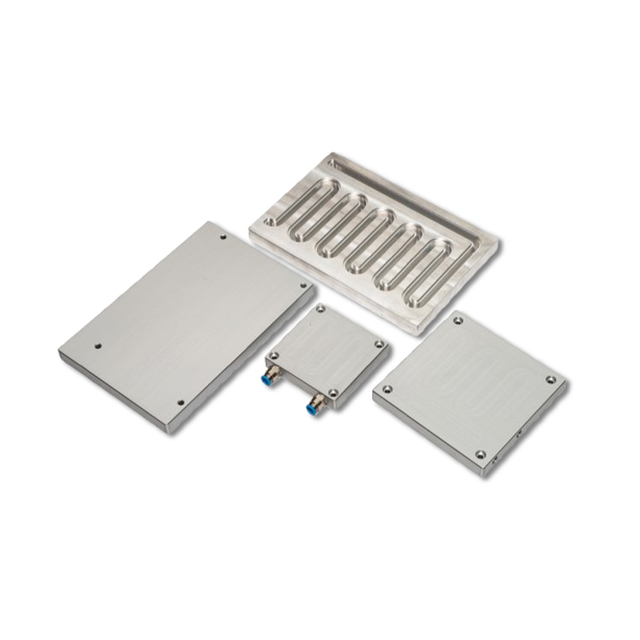
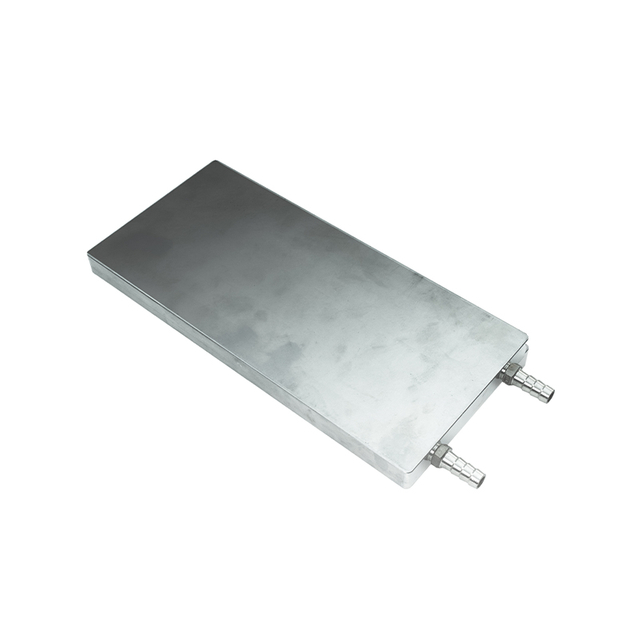
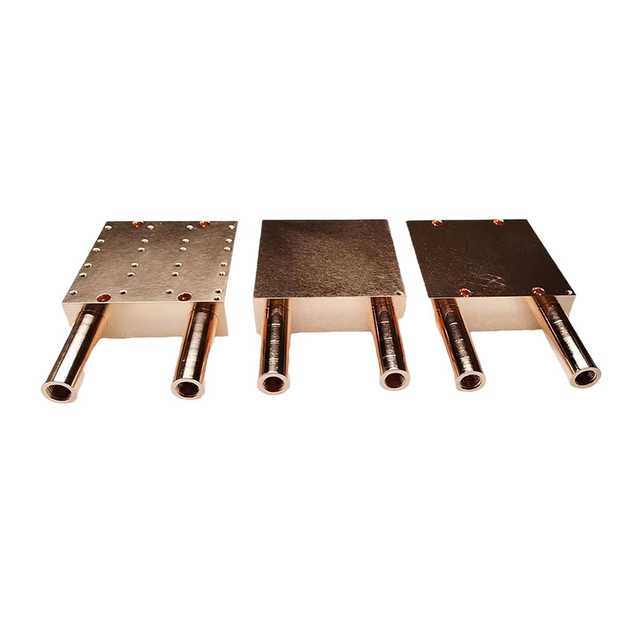
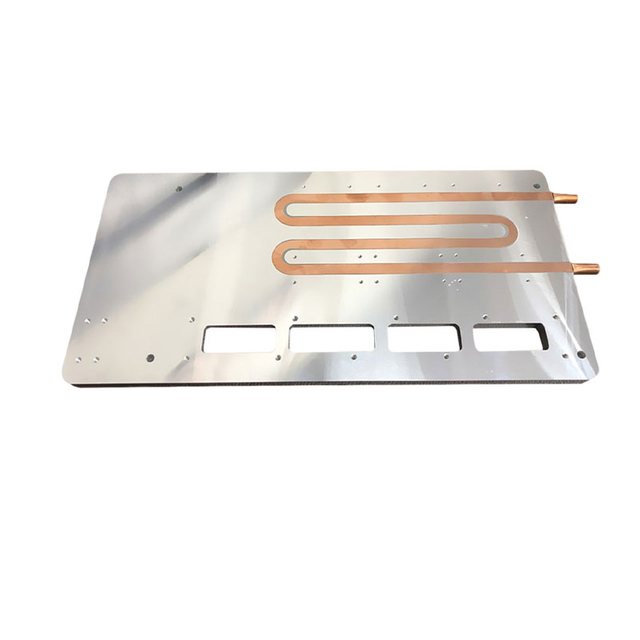
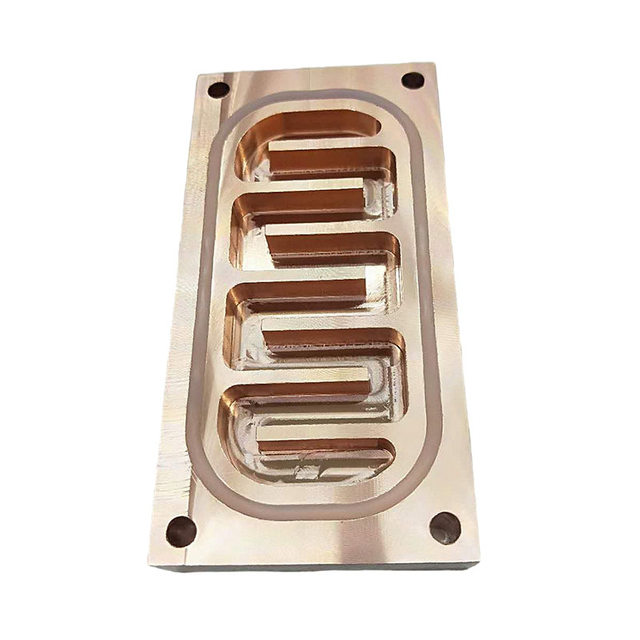
An Aluminum 6061/6063 base is CNC-milled with coolant channels matched to the converter or controller heat load, then sealed by a solid-state FSW cover. The layout targets the high-loss power devices directly, and the flat mounting face keeps thermal contact stable across temperature swings. Finish options support corrosion resistance for demanding environments.
Sized for EV, ESS, solar and wind power-conversion heat loads.
Solid-state joints stand up to thermal cycling and pressure.
Channels routed to high-loss semiconductors.
Surface treatment options for harsh duty.
Airtightness and flow validation on every plate.
Base Plate Material | Aluminum 6061/6063 |
|---|---|
Cooling Circuit | CNC-machined channels, solid-state FSW-sealed |
Joining Technology | Solid-state Friction Stir Welding (FSW) - no flux, no filler metal |
CNC Machining Tolerance | As tight as +/-0.005 mm (high-speed milling / turning) |
Dimensional Inspection | Hexagon CMM +/-0.001 mm; 2.5D optical projector |
Leak Testing | 100% airtightness leak detection (4 x LCP leakage testers) |
Flow Validation | Two-stage flow-resistance test |
Surface Control | Fly-cut / ground mounting face; Kett film-thickness & roughness testers |
Quality System | ISO 9001:2015; IATF 16949:2016 |
Coolant Handling | Airtight-cleaned, residue-free channels; coolant matched to your system |
Lead Time | Typical samples 7-15 days; production scheduled to volume |
Note: the table lists KingKa's verified build options and capabilities. Final geometry, passes, ports and finish are confirmed against your drawing.
KingKa controls every step of the build in-house, from incoming-material inspection to final flow testing. The workflow below reflects the FSW construction used for this liquid cold plate.
Thermal design & DFM. 3D Pro/E layout and CFD review of the internal channels before any metal is cut, so the flow path matches your heat map and pressure-drop budget.
CNC channel machining. Channels, fins and port features are milled in the aluminum or copper base on 50+ CNC centers (3-/4-/5-axis), then the cover plate is positioned for welding.
Friction Stir Welding. A rotating tool forges the cover to the base below the melting point on two China-Aerospace FSW machines - a flux-free, solid-state seal with no porosity path.
Finish & validation. The welded plate is fly-cut flat, then every assembly passes 100% airtightness leak detection and a two-stage flow-resistance test before CMM dimensional sign-off.
100% airtightness leak detection - four dedicated LCP leakage testers confirm every assembly.
Two-stage flow-resistance test - channels are clear and pressure-stable.
Hexagon CMM & 2.5D projector - dimensional verification to +/-0.001 mm against your drawing.
Airtight internal cleaning - residue-free channels ready for your coolant.
Salt-spray & Kett film/roughness - corrosion and surface-finish validation per batch.
These water cooling plates serve the demanding thermal duty of new-energy and electronic systems:
EV drivetrain and on-board chargers
Battery energy storage systems
Solar inverters and wind converters
Motor controllers and drives
Industrial power conversion
Provide your power-stage layout, envelope, coolant and duty cycle. KingKa designs the channel network and manufactures the FSW cold plate to your drawing, with validation to match your operating conditions.
For buyers, KingKa is a direct manufacturer with 16+ years of thermal-production experience, 50+ CNC centers (3-/4-/5-axis) and a stated 60,000+ parts per year, certified to ISO 9001:2015 and IATF 16949:2016. Engineering support includes in-house CFD thermal simulation and 3D design before tooling.
From drawing to volume. Send your STEP/CAD file and thermal budget for a CFD-backed proposal.
Flexible supply. Prototypes typically 7-15 days; production scheduled to your forecast.
One quality system. Prototype, pilot and production all carry 100% leak and CMM inspection.
R&D backing. Dongguan Nancheng R&D center supports design, validation and scale-up.